A tablet strip packing machine feeds tablets or capsules between two heat-sealable webs, seals around each dose, and cuts the material into finished strips. Choose the feeder, sealing tools and strip layout around your product and required accepted output.
Comwin develops tablet and capsule packaging solutions from a single packing machine to a coordinated production line. We match product feeding, sealing, inspection and downstream handling to your product, factory and growth plan.
Price guide: For early planning, allow US$20,000–45,000 for a conventional automatic strip machine, US$35,000–75,000 for more demanding feeding and inspection, or US$70,000–150,000 for a strip machine linked to basic cartoning. These are conditional planning estimates, not quotations. See what each budget includes.
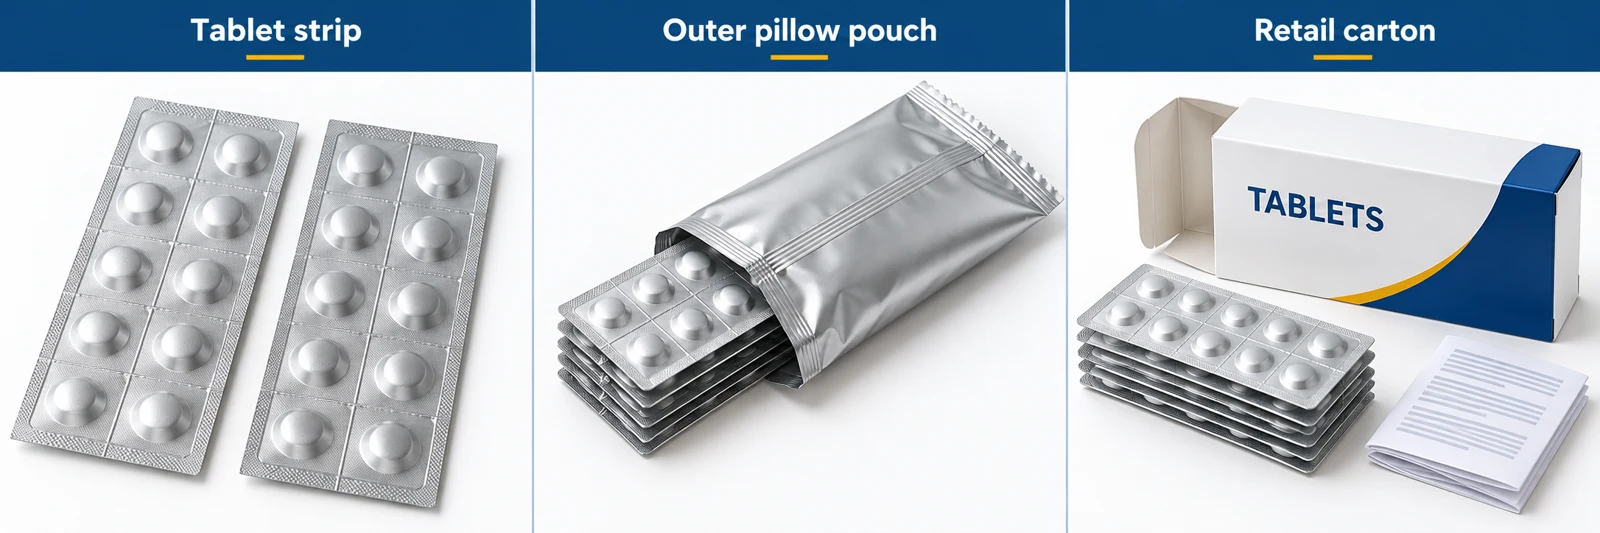
Which tablet strip packing configuration fits your product?
Send your product sample, finished-strip drawing and required daily output. If the pack is not yet fixed, we can recommend its layout alongside the machine. The useful starting choices are the following production configurations.
| Your product and finished pack | Recommended equipment | Why this configuration fits |
|---|---|---|
| Regular tablets in repeat strip formats | Automatic tablet strip packing with product-specific feeding tracks, matched seal tools and the required cut/perforation pattern. | Coordinated feeding and web sealing suit repeat production. Track count and strip length follow the dose arrangement and output target. |
| Hard capsules, oblong tablets or fragile products | A capsule strip packing machine or tablet strip machine with a feeder and clearances tested for the product; inspection and rejection where required. | Orientation, product thickness and transfer contact can determine whether doses reach the sealing area correctly. A faster drive alone does not solve difficult feeding. |
| Finished strips grouped into retail cartons | Strip packing linked to counting/stacking, transfer and a retail cartoner, with leaflet handling as specified. | Use this when pack grouping or cartoning is the bottleneck. Size the transfer and cartoner for the number of strips per carton. |
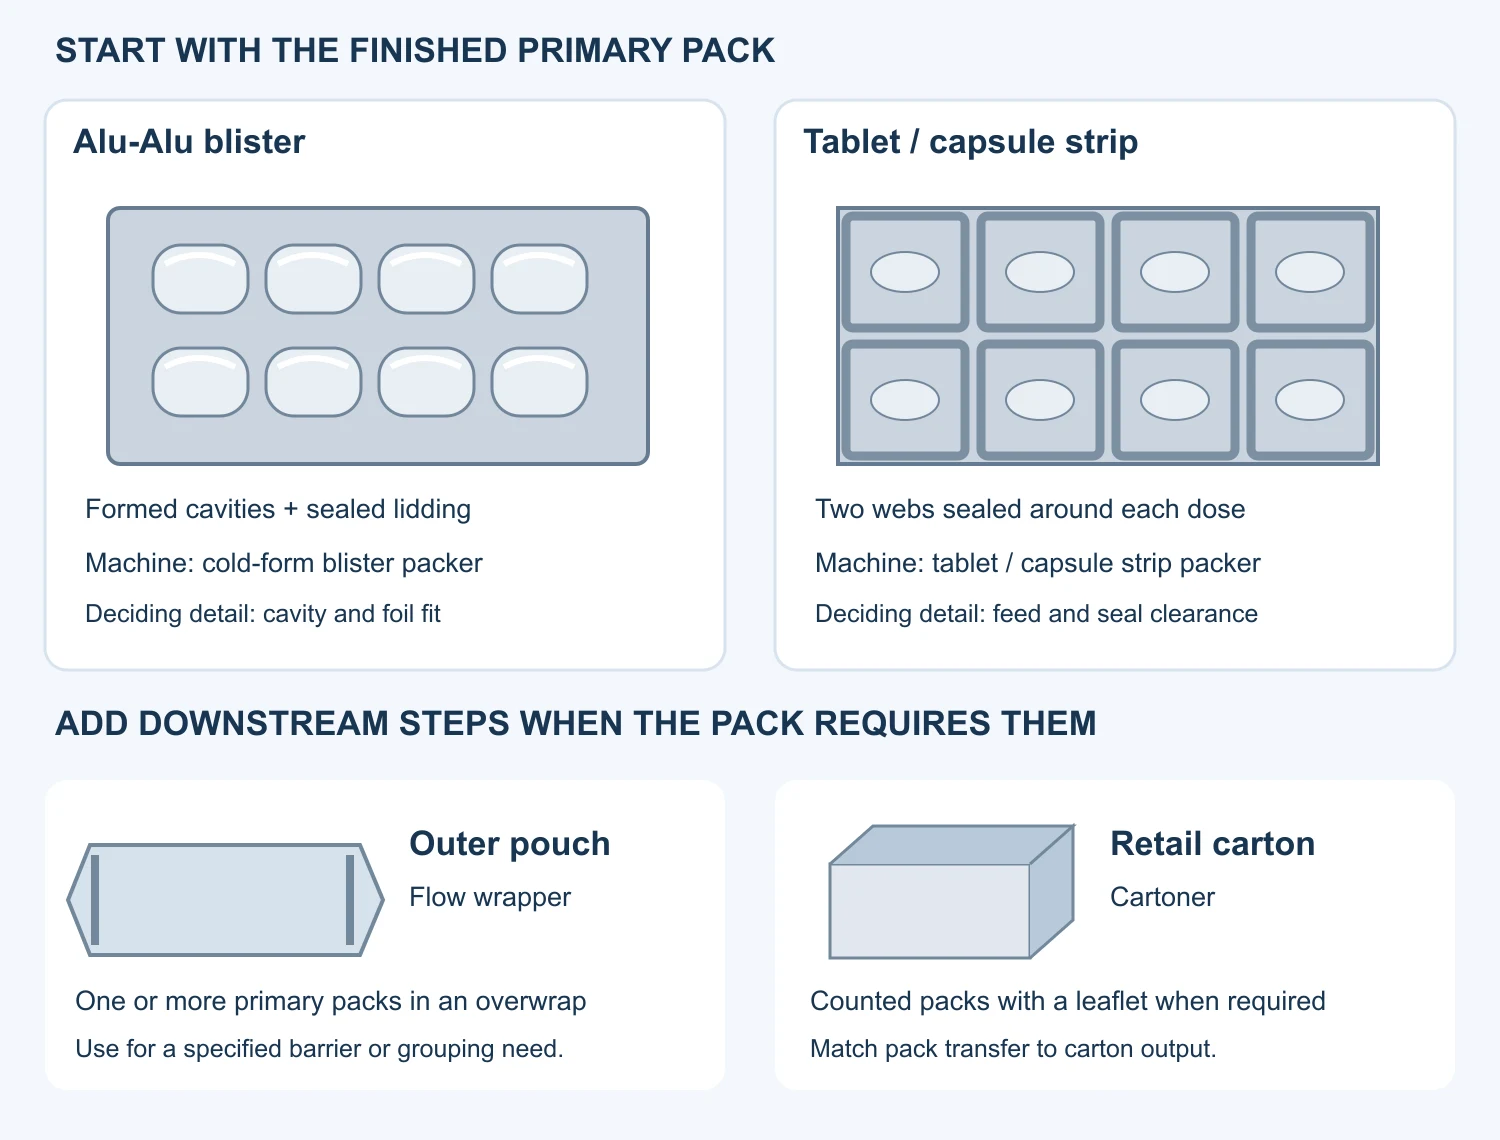
| A pack drawing requires individual cold-formed cavities | A cold-form blister route rather than strip sealing. | The required primary pack is different. See the short strip-versus-blister comparison before specifying equipment. |
We use your samples to determine whether the feeder, sealing arrangement and change parts fit the job. You do not need to decide the machine modifications in advance.
Solve the strip-packing problem with the right configuration
| Problem to address | Recommended configuration or action | How it helps; what to check |
|---|---|---|
| Broken tablets, capsule jams or doses trapped in the seal | Product-specific feeder tracks, gentle transfer and synchronized delivery into the sealing tools. | Give the product enough clearance and avoid uncontrolled drops. Run representative samples and inspect breakage and trapping at normal speed and after restarts. |
| Weak seals, wrinkles or seals contaminated by product dust | Compatible coated webs, stable web guidance/tension, controlled sealing conditions and appropriate dust management. | These address the material/process interface. Check seal quality and pack integrity with the actual webs; a foil description alone does not establish shelf life. |
| Missing doses, unreadable printing or misplaced cuts | Suitable dose-presence detection, print registration/coding and inspection with confirmed rejection. | Specify which defect must be detected and where. Challenge missing-dose, coding and reject behavior; do not assume every feature is included in a base machine. |
| Frequent formats or slow carton grouping reduce shift output | Documented change parts and repeatable settings; add strip counting/stacking and cartoning when downstream handling limits output. | Compare cleaning-to-first-good-strip time and accepted carton output. Test recovery when either upstream or downstream equipment stops. |
Tablet and capsule strip-packing applications
| Production situation | Finished pack | Recommended configuration | Information that determines the fit |
|---|---|---|---|
| Repeat batches of coated oral tablets | Printed strips with the specified dose count | Automatic tablet feeding, registered web sealing and cutting. | Tablet dimensions, coating behavior, doses per strip, print repeat and accepted output. |
| Hard capsules that require controlled orientation | Capsule strips with adequate product clearance | Capsule-specific feeding and seal tools, with product-presence inspection where specified. | Capsule size, orientation, clearance, handling damage and tear/cut arrangement. |
| Fragile tablets with frequent SKU changes | Short runs in several strip formats | Gentler product handling and accessible, repeatable format changes. | Breakage during trials, batch size, cleaning requirements and the parts changed for each SKU. |
| Retail packs containing several strips and a leaflet | Counted strips in a closed carton | Strip packing, counting/stacking, transfer and cartoning. | Strips per carton, carton dimensions, leaflet specification and sustained line output. |
Example: hard capsules sold in ten-dose strips
We start with the capsule dimensions and a ten-dose pack drawing. Feeding orientation, track layout and space around each capsule determine the sealing tools. If five strips go into one carton, downstream equipment must count five acceptable strips, transfer them without losing the grouping, and coordinate with carton loading. This example defines the pack counts needed to size the transfer and cartoner.
Example: fragile tablets made in short batches
Here, gentle feeding and repeatable cleaning/changeover may matter more than maximum running speed. Compare the time to the first acceptable strip after a format change, as well as breakage during a representative run. Automatic cartoning becomes useful when manual grouping cannot keep pace with the required saleable output.
Tablet strip packing machine prices and line budgets
Use the following ranges to set an initial equipment allowance. They apply to routine oral-solid tablet/capsule projects supplied from China, with one strip format and basic factory setup. The three strip budgets overlap because configuration and output requirements vary.
| Equipment scope | Budget, USD | Scope behind the allowance |
|---|---|---|
| Conventional automatic tablet/capsule strip machine | $20,000–45,000 Planning estimate | Routine product feeding, two-web sealing, cutting, basic controls and one set of format tools. The offer must identify coding, guarding and any included checks. |
| Strip machine with enhanced feeding and inspection | $35,000–75,000 Planning estimate | Allowance for product-specific feeding, selected servo/control functions and specified detection/rejection. These are quotation items, not a promise that every option is included. |
| Strip packing linked to basic automatic cartoning | $70,000–150,000 Combined planning estimate | Primary strip machine, transfer/grouping and basic cartoning coordination. The strip machine is already included; more complex lines can exceed this range. |
| Automatic retail cartoner added to existing primary packing | $25,000–80,000 Comwin budget reference | Small-carton equipment allowance. Specify strip stacking, leaflet handling and interfaces. Shipping-case packing is a separate operation. |
| Optional flow wrapper for an outer pouch | $5,000–25,000 Comwin budget reference | Overwrap around already sealed primary packs, where required by the pack specification. It is not the tablet strip machine. |
Budget basis: Strip ranges are AI-assisted planning estimates reviewed on October 5, 2026, not verified market averages or Comwin quotations. Cartoner and flow-wrapper references come from Comwin’s September 4, 2026 budget table. Confirm the selected functions in the itemized quotation. The estimate excludes freight, import taxes/duties, overseas installation/travel, additional formats, consumables and extensive validation/traceability requirements. High-speed or difficult-product projects need separate configuration review. Confirm inclusion of tooling, coding, inspection, training, spares and documentation, and compare quotations on the same EXW, FOB or CIF basis.
To control investment: Start with the required product/strip format, budget the additional format parts explicitly, and automate the measured bottleneck. Do not add a separate strip-machine price to a combined line allowance that already includes it.
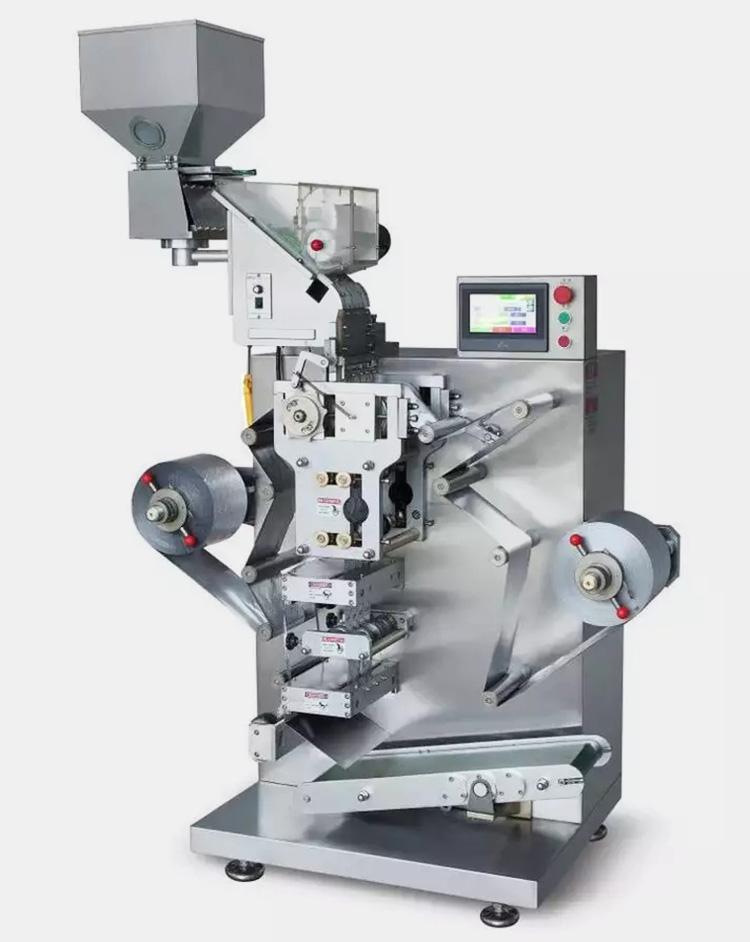
How a tablet strip packing machine works
- Feed and orient the product. A suitable feeding arrangement delivers tablets or capsules at the required spacing.
- Guide the two webs. The heat-sealable materials pass through the web path; printed material needs registration matched to the pack repeat.
- Seal around the doses. Matched tooling and controlled sealing conditions close the webs around each dose, with clearance for its shape and thickness.
- Code, perforate and cut as specified. Produce the required strip count and tear arrangement. Coding location and inspection order follow the machine layout.
- Inspect and discharge accepted strips. Detection/rejection is specified for the relevant defects. Discharge to collection, grouping, overwrapping or cartoning as required.
Machine layouts differ. Ask for the proposed process diagram and identify the point where each required defect is checked. A strip sealing machine must coordinate product delivery, web position, heat sealing and cutting—not simply seal two empty films.
Match the foil and seal pattern to the product
Strip systems can use compatible aluminum-based laminates or other specified heat-sealable webs, depending on the selected equipment and package. Confirm both sealing surfaces, material thicknesses, print repeat and the required product barrier. Do not treat “aluminum foil” as a complete material specification.
For moisture-sensitive tablets, review the material barrier and test the finished pack under the product’s protection requirements. For large or thick capsules, give the sealing tools sufficient clearance. Perforations and cut edges must support the required opening method without interfering with the sealed dose area.
Include representative product and printed webs in the trial. Check product placement, seal condition, print/cut alignment, roll-change setup and restart behavior. Product stability or shelf-life claims require appropriate evidence beyond the machine trial.
Size output in doses, strips and cartons
A machine figure stated in tablets per minute cannot be compared directly with strips per minute. Record the doses per strip and strips per carton before comparing offers.
Worked planning example: To deliver 360,000 accepted doses during six productive hours, you need 1,000 accepted doses/minute. At ten doses per strip, that is 100 accepted strips/minute. At five strips per carton, downstream handling needs 20 accepted cartons/minute before allowing for downstream rejects or interruptions.
This is a sizing example, not a Comwin machine rating. Productive hours exclude planned cleaning and changeovers; account separately for rejects and interruptions rather than counting the same loss twice. Specify your required accepted shift output, then test the selected configuration with your product and webs.
Compare manual work, automatic strip packing and a linked line
| Production pattern | Machine and operator work | Changeover and upkeep | Output to compare |
|---|---|---|---|
| Trials or short batches | A suitable trial/low-volume sealing arrangement, with the required manual product loading or pack transfer. | Accessible tools, repeatable settings and practical cleaning. A hand sealer alone may not feed, register or cut the finished strip. | Repeatable pack quality and acceptable batch output. |
| Repeated strip production | Automatic product feeding, sealing and cutting; operators replenish product/webs and handle exceptions. | Include feeder cleaning, format parts and first-good-strip setup in shift planning. | Accepted strips/minute and doses per shift with actual materials. |
| Strips packed into retail cartons | Automatic grouping and cartoning where required; operators replenish cartons/leaflets and manage the line. | Coordinate format settings, stop signals, accumulation and restart across machines. | Accepted cartons/minute at the specified strips-per-carton ratio. |
Add overwrapping and cartoning for a defined pack requirement
Finished strips can discharge for collection. Use a flow wrapper if the finished-pack specification calls for an outer pouch around one or more strips. Use a cartoner when strips must be counted and placed into retail boxes, with a leaflet where required. Shipping-case packing follows when that operation belongs in the project.
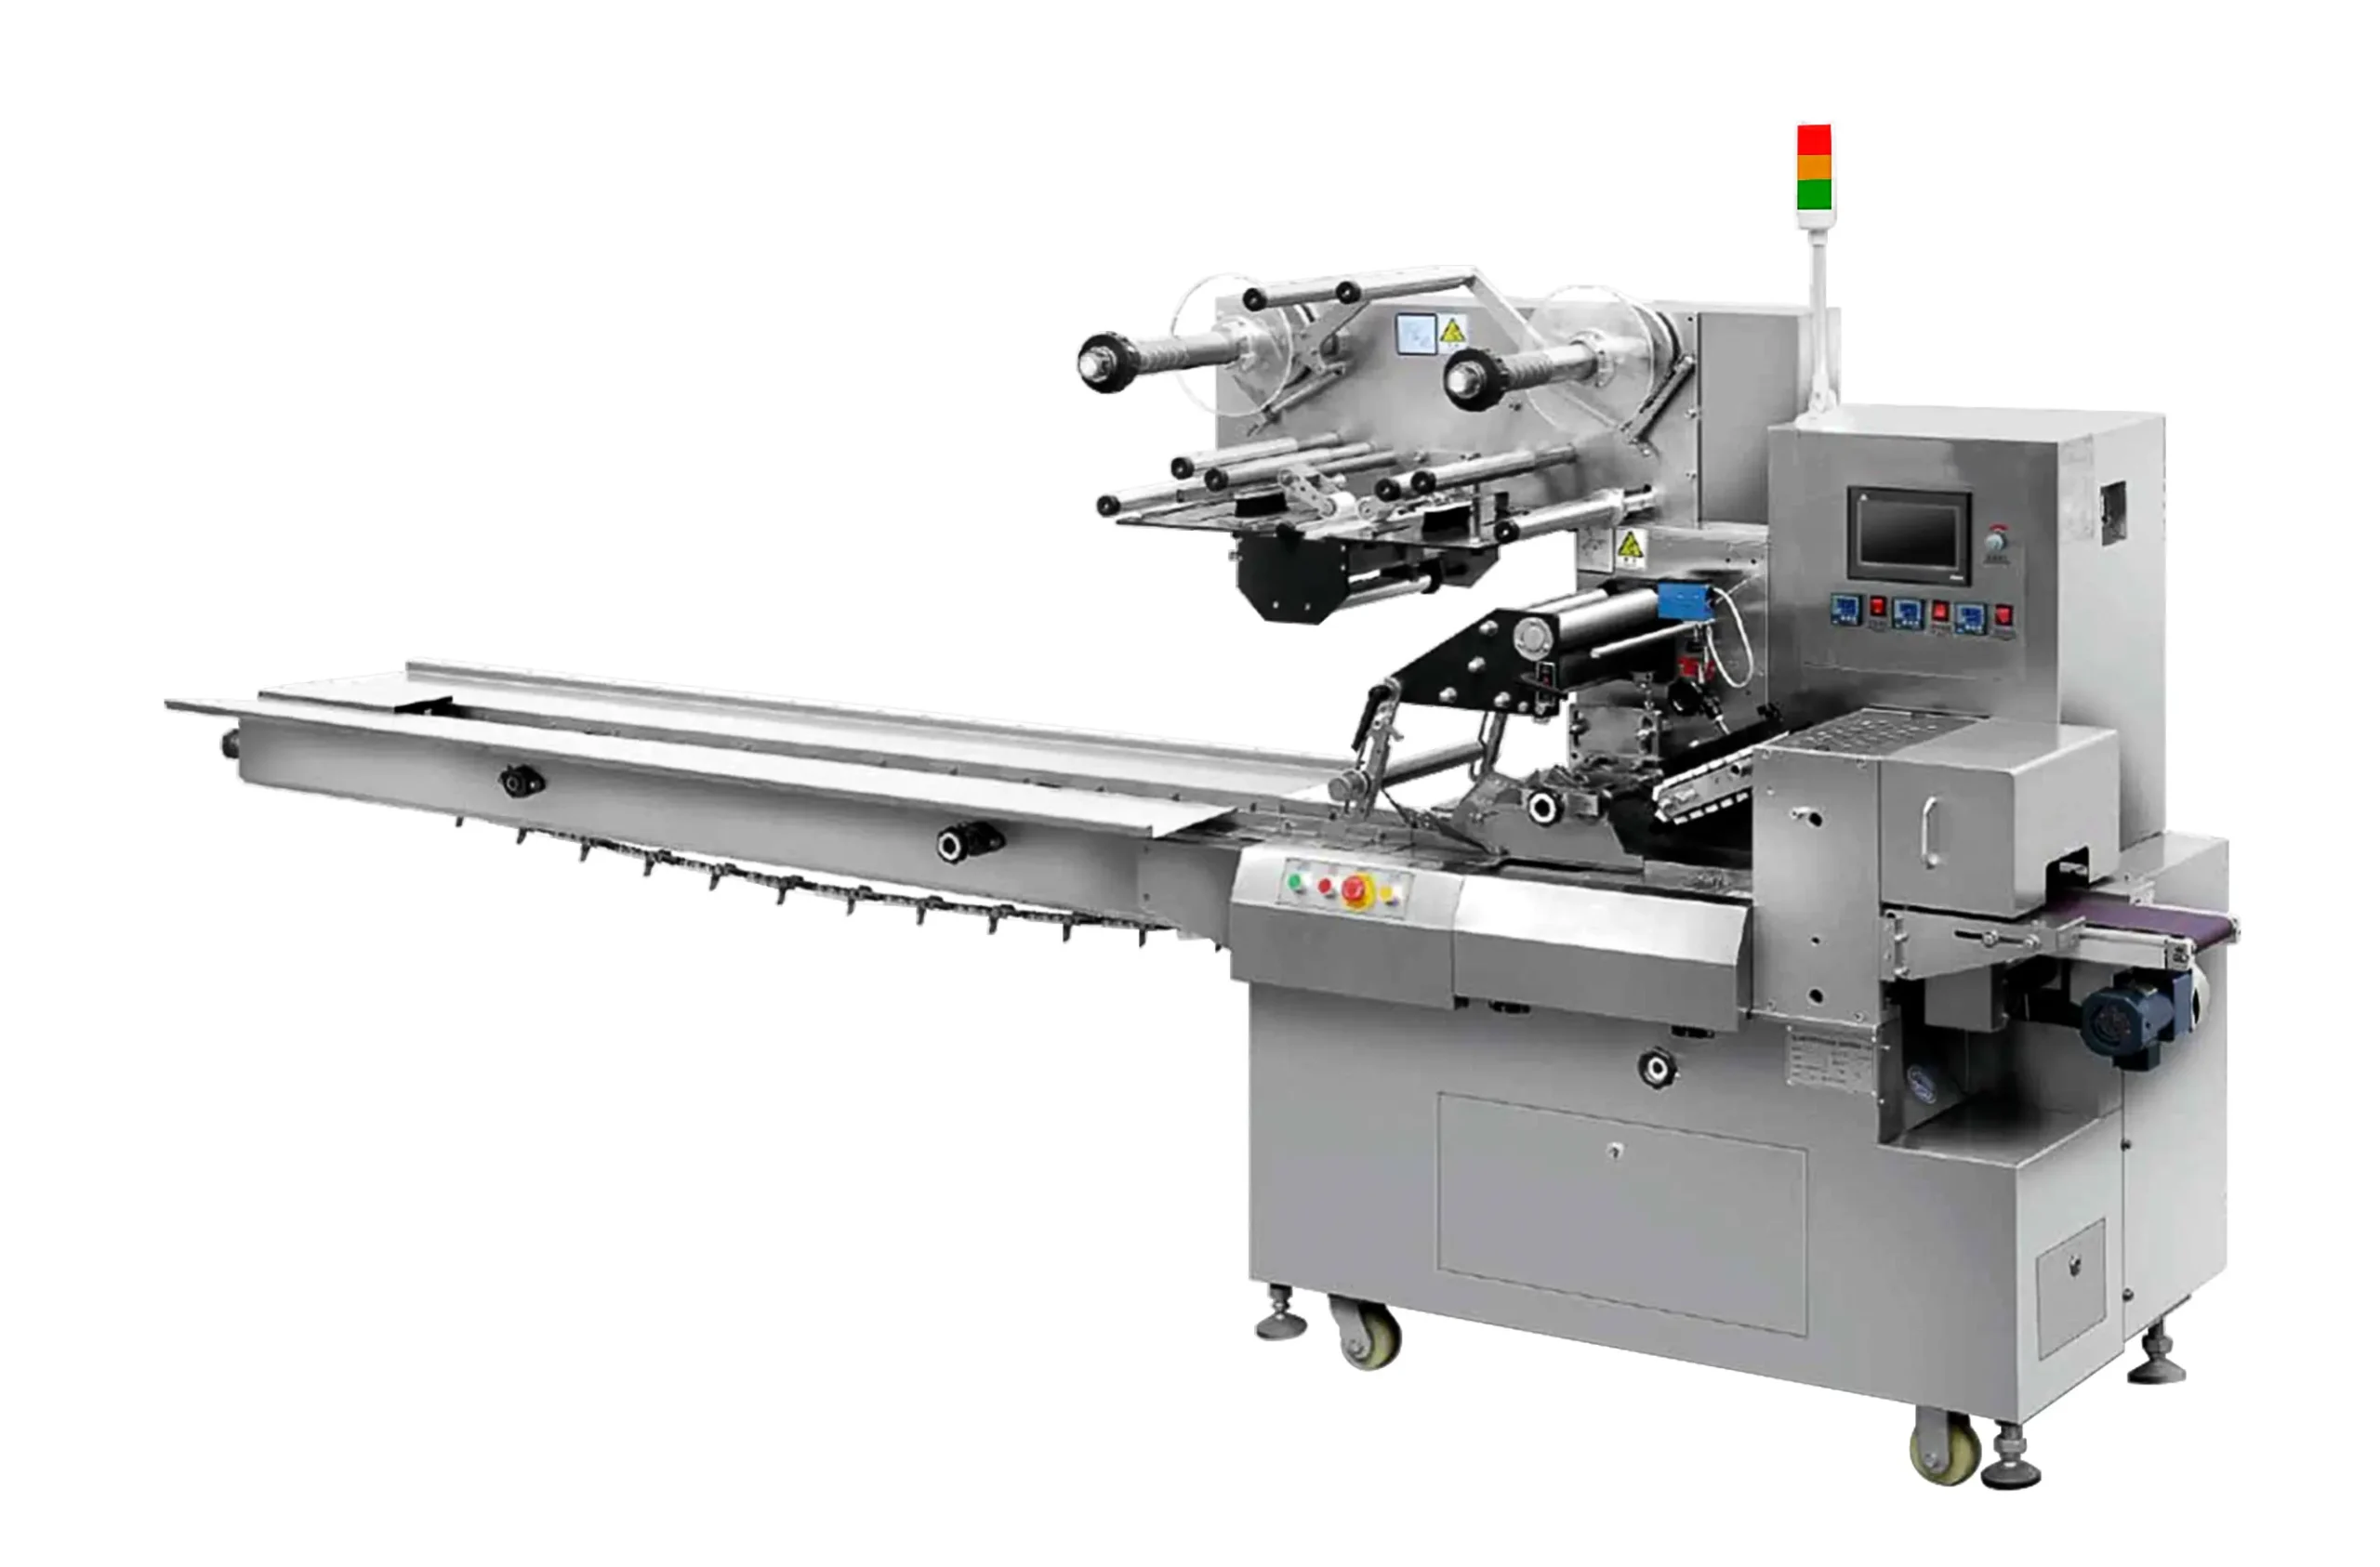
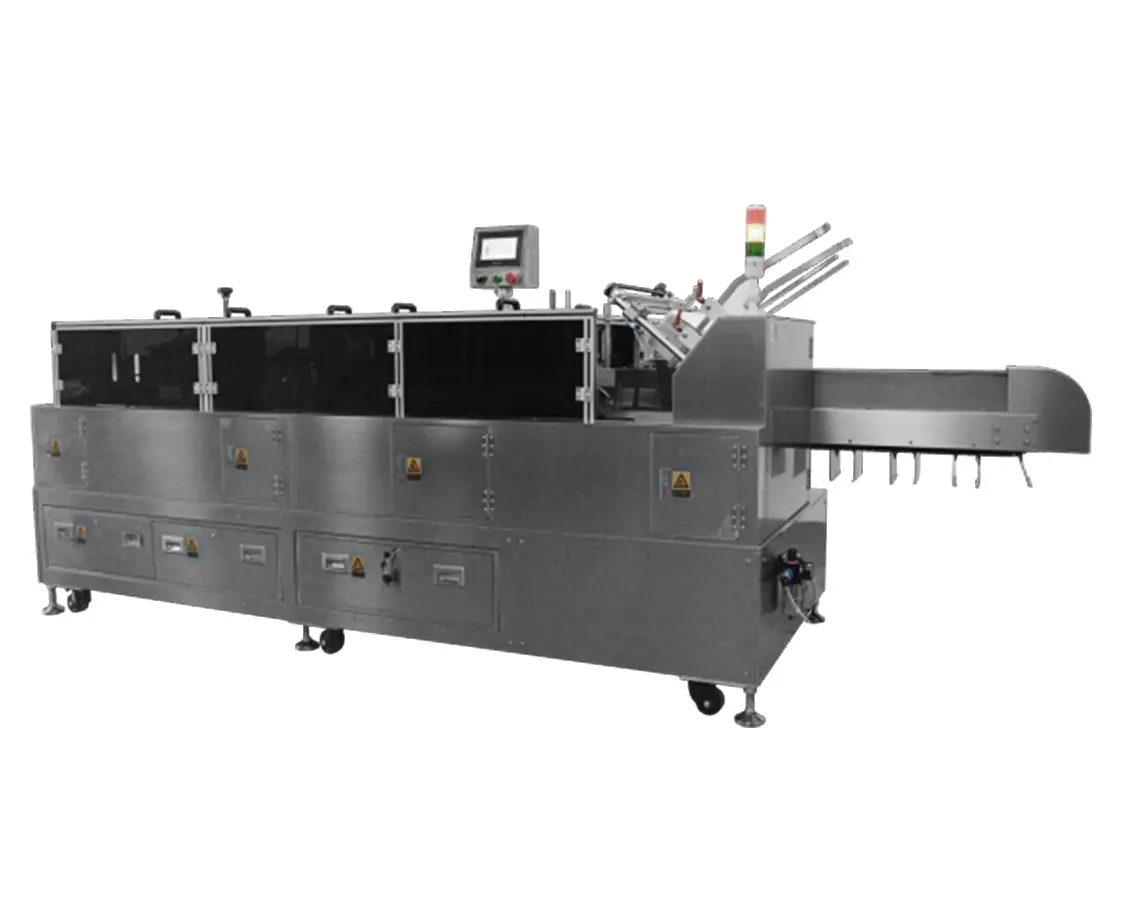
The line design must define how strips are counted, accumulated and transferred, and what happens when a machine stops. Match these interfaces to the actual carton count; a conveyor alone does not balance output.
Compare cost per acceptable finished pack
Compare both web areas consumed per strip from the pack drawing, including seal margins, trim and startup waste. Add labor, utilities, maintenance and allocated equipment cost over the same period, then divide by acceptable saleable packs. Use the same unit: a strip and a carton of several strips are different products.
For many short batches, cleaning, format changes and startup rejects may dominate the comparison. For longer runs, sustained accepted output and material yield become more important. Calculate whether downstream grouping limits production before investing in additional primary-machine speed.
When is a blister machine the better fit?
Choose the blister route if your product presentation requires separately formed cavities sealed with lidding material. Strip packaging seals around the product between two webs; an Alu-Alu blister requires cold-forming capability and its own tooling. Both can use aluminum-based material, so the material name alone does not identify the process.
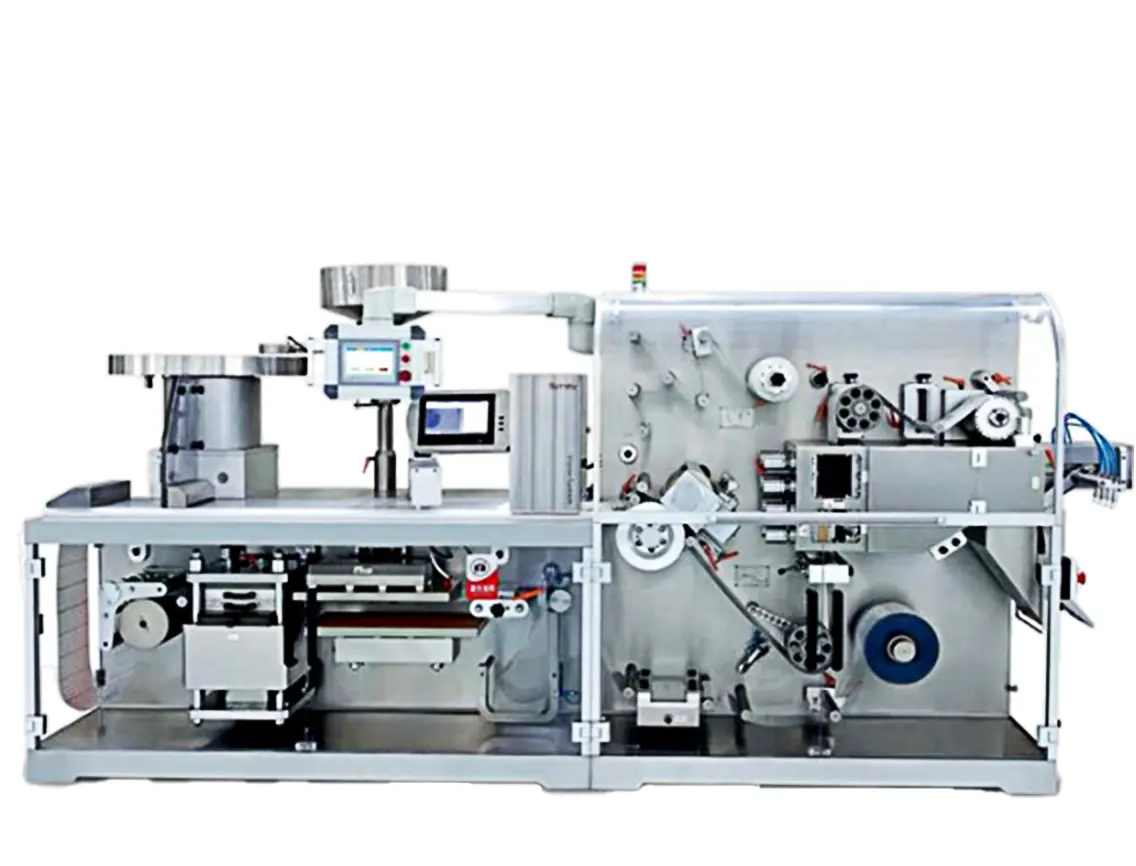
Comwin’s general blister-machine budget reference is US$20,000–60,000; it does not establish the price or capability of a particular Alu-Alu cold-form configuration. Review the blister packaging route if your approved pack requires cavities. Neither process is automatically cheaper or more protective for every product.
Compare suppliers on the same strip-packing project
| Decision | What we establish for your project | How to compare another offer |
|---|---|---|
| Budget and supply scope | Match product feeding, format tools, inspection and downstream equipment to the required strip. | Compare included items and delivery terms, not just the headline price. |
| Production scale | Translate daily doses and pack counts into accepted strip/carton targets. | Check units, product conditions, shift assumptions and trial criteria. |
| Product and format changes | Identify feeder changes, seal/cut tools and setup tasks for your SKUs. | Request a change-parts list and a representative changeover demonstration. |
| Support and documentation | Agree operating guidance, maintenance information and project documentation. | Confirm response scope, training arrangements, spares and required records. |
| Delivery and acceptance | Define the selected configuration and acceptance run with your product and packaging material. | Compare contractual milestones and evidence for accepted output and pack quality. |
Tablet strip packing machine FAQ
How much does an automatic tablet strip packing machine cost?
For a routine one-format project, use US$20,000–45,000 as an initial planning estimate. If feeding, inspection or controls are more demanding, the US$35,000–75,000 allowance may be more relevant. Compare included functions and product-trial requirements before treating two prices as equivalent.
Can one strip machine run both tablets and capsules?
If the selected machine can accommodate both products, the feeder, tracks and sealing/cutting parts may need changes. Send representative samples and pack drawings for free sample testing; the results guide the common configuration and format parts. Similar dimensions alone do not prove shared tooling.
Is a strip machine the same as an Alu-Alu blister machine?
No. If the pack requires preformed cavities, specify a suitable blister machine. If doses are sealed between two webs, specify a strip packing machine. Use the finished-pack drawing to identify the process before comparing equipment prices.
Does manual strip packing make sense for small batches?
For trials or occasional batches, consider a suitable low-volume process when it can reproduce the required seal and pack layout. If you need repeat registration, controlled dose placement and predictable shift output, evaluate automatic strip feeding and sealing. Check the whole finished-strip process, not only a hand sealer’s purchase price.
When should automatic cartoning be added?
When strip counting, grouping or carton loading limits required saleable output, evaluate a linked cartoner. For five strips per carton, divide accepted strip output by five, then allow for downstream losses and interruptions. If manual handling already meets the target, budget improvements around the actual bottleneck.
Is this suitable for pharmacy medication sachets?
If you need patient-specific medication doses packed into labeled sachets, specify that dispensing workflow separately. Industrial tablet/capsule strip packing described here is a different task; do not select equipment solely because both are called pill packaging.
Get a tablet strip-packing proposal from Comwin
Send the following information so we can recommend feeding, strip format, inspection and downstream equipment together:
- Product: tablet/capsule samples, dimensions, shape and handling concerns.
- Finished strip: drawing or sample, doses per strip, tear/perforation requirements and print layout.
- Materials: both web specifications, roll dimensions and relevant protection requirements.
- Production: daily acceptable doses/packs, shift hours, SKUs and batch/changeover pattern.
- Downstream: collection, outer pouch or carton requirements; strips per carton and leaflet specification.
- Factory and delivery: available space, utilities, destination, trade terms and documentation needs.
Comwin provides product-based equipment matching, free sample testing and support for single machines through coordinated lines. We can arrange factory inspection and agree training and support for the selected scope.
Send your product and strip-pack requirements to receive a proposed equipment scope, format/change-part plan and itemized quotation.