
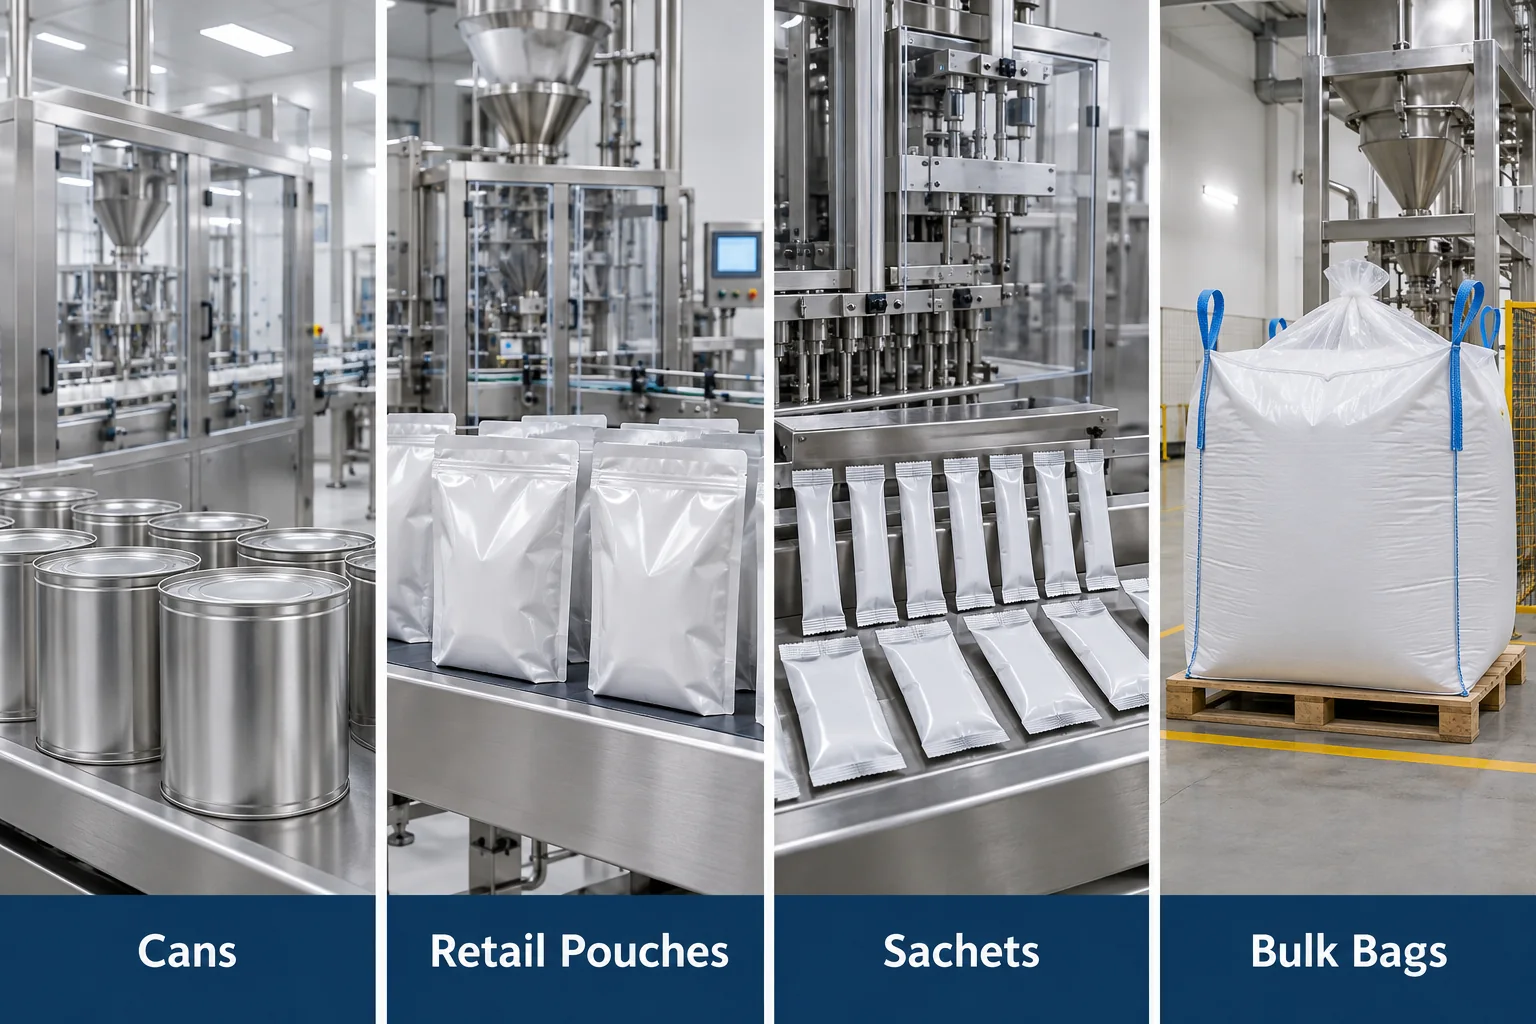
Select the Finished Milk Powder Package
Package choice determines the dosing, atmosphere and closing system. Rigid cans protect the powder and provide room for a scoop but require lid handling and seam validation. Roll-film pouches reduce package weight and storage volume. Sachets serve single portions but add multiple narrow product and seal paths. Bulk bags need dust-tight docking, accurate weighing, densification and liner closure in the defined hygiene zone.
| Pack | Primary machine route | Best fit | Confirm first |
|---|---|---|---|
| Metal or composite can | Auger/net-weight filling, optional gas control, lid placement and compatible closing system. | Premium retail, nutrition and high-barrier packs. | Can/end drawings, fill weight, scoop, headspace, gas target and closure test. |
| Retail VFFS pouch | Roll-film forming, powder dosing, deaeration, optional gas flush, sealing and cutting. | Common consumer and foodservice bags. | Film, bag style, bulk density, dose, gas and seal window. |
| Sachet/stick pack | Single/multilane form-fill-seal with per-lane powder dosing. | Samples, single servings and institutional portions. | Lane count, dose, powder flow, web registration and seal cleanliness. |
| Open-mouth or FIBC bag | Hygienic bag docking, gross/net weighing, dust extraction, settling and liner closure. | Industrial ingredient supply measured in kilograms. | Bag/liner, target weight, pallet policy, room boundary and sealing. |
Powder Behavior Determines Dosing
Milk powder can change apparent volume after transport, conveying and settling. Bulk density, entrained air, particle size distribution, fat content and humidity affect how it flows and how much space a target weight occupies. Measure loose and settled bulk density from production material rather than using a generic value.
Powder should travel through enclosed, cleanable equipment with controlled dust collection. Excessive agitation or long drops can create dust and segregation; insufficient venting can inflate a pouch or cause powder to escape during filling. The line must also be assessed for combustible-dust risk under the rules applicable to the installation site.
| Property | Machine effect | Test or input |
|---|---|---|
| Loose/settled bulk density | Changes volumetric dose, headspace and bag/can capacity. | Minimum/maximum production density and settling behavior. |
| Flowability/cohesion | Changes auger feed, bridging and refill stability. | Angle/flow observations, stoppage behavior and hopper geometry. |
| Aeration | Causes apparent-volume drift, dust and pack expansion. | Deaeration/settling trials and weight recovery after fill. |
| Moisture/fat sensitivity | Raises sticking and cleaning needs; affects package barrier. | Product specification, room humidity and storage study. |
| Combustible-dust data | Changes extraction, grounding, zoning and equipment protection. | Site hazard assessment and applicable ATEX/NFPA/local requirements. |
Choose Auger, Net-Weight or Combination Dosing
| Dosing method | Suitable case | Advantages | Validate |
|---|---|---|---|
| Servo auger | Repeatable powders and retail can/pouch/sachet doses. | Compact metering with recipe-controlled screw revolutions. | Auger/tooling, density change, cutoff, refill and cleaning. |
| Net-weight filler | Weight-critical retail or bulk formats with stable controlled flow. | Direct measurement and coarse/fine feed control. | Scale resolution, vibration, air movement, settling and cycle time. |
| Auger with checkweigh feedback | Automated retail line with predictable correction strategy. | Combines fast dosing with trend correction. | Sampling frequency, rejected packs and limits of feedback control. |
| Gross-weight bulk filling | FIBC or large open-mouth bag weighed during fill. | Bag and contents weighed as one controlled package. | Tare, suspension/pallet arrangement, coarse/fine cutoff and legal metrology. |
Four Milk Powder Packaging Routes
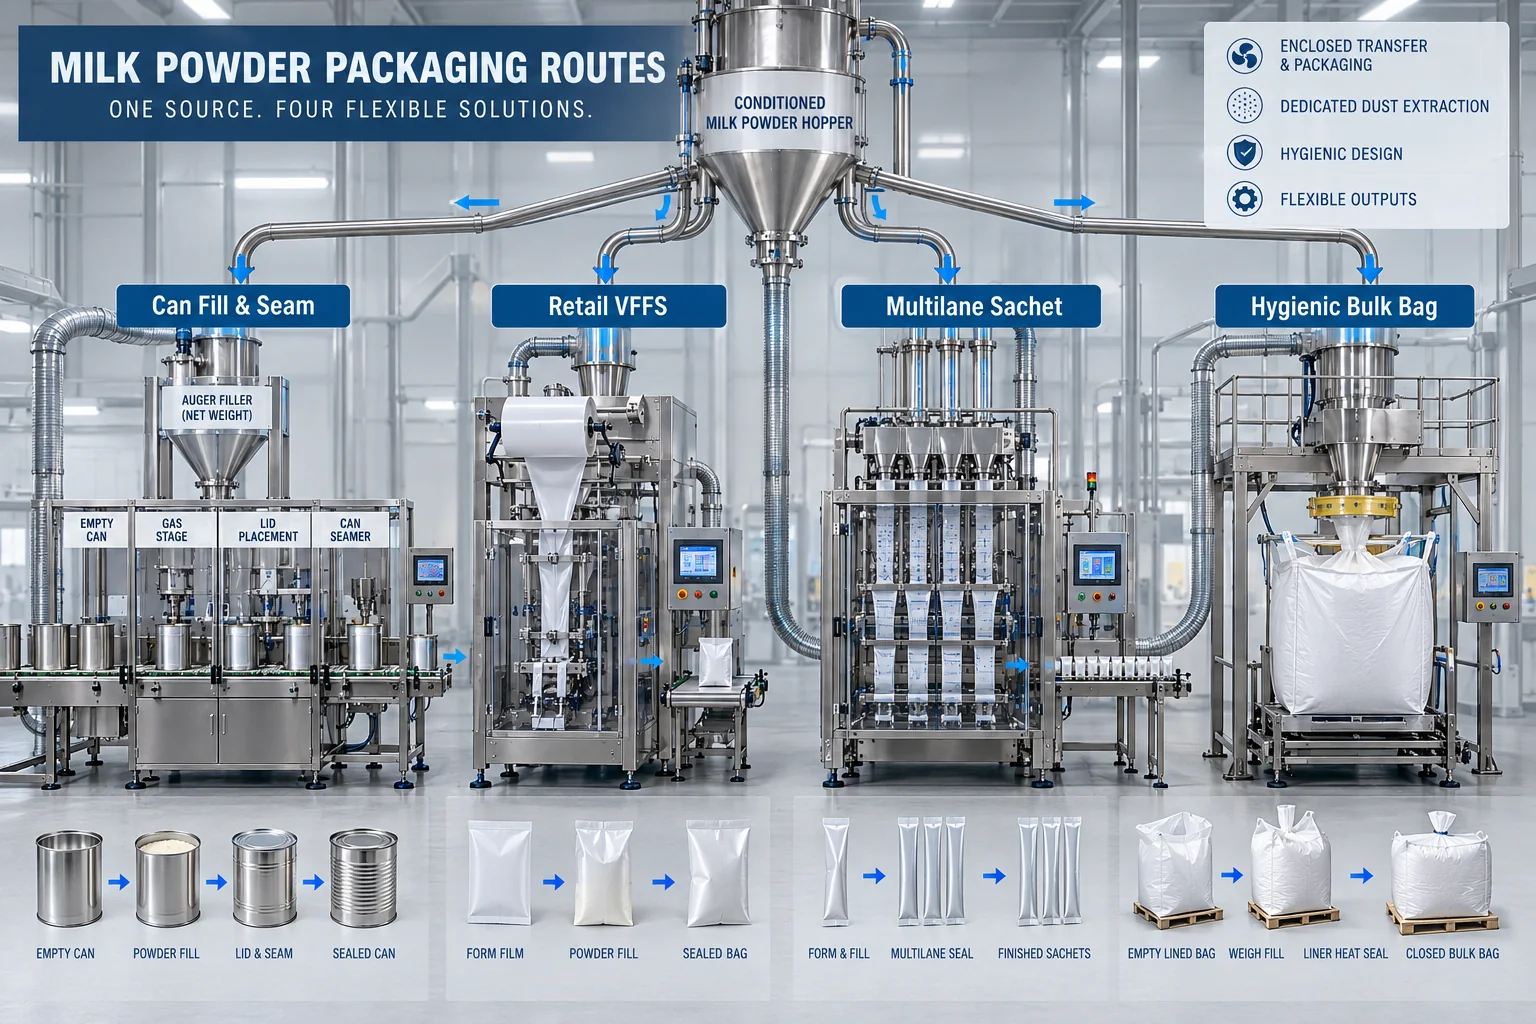
The routes may share an enclosed powder source, but they need different primary machines. Can filling ends at a compatible seam or closure. VFFS forms the retail bag from roll stock. Multilane equipment forms several small sachets in parallel. Bulk systems dock and weigh-fill a lined bag, then close the liner before it leaves the controlled area. Define upstream powder screening/metal control and downstream code, inspection and case or pallet handling separately.
| Route | Machine inlet | Accepted outlet | Common options |
|---|---|---|---|
| Can fill and seam | Empty qualified can, powder, lid/end and optional scoop. | Correct-weight sealed can meeting seam/atmosphere criteria. | Can cleaning/treatment, gas, residual-O₂, label, case pack. |
| Retail VFFS | Conditioned powder and qualified barrier roll film. | Sealed coded pouch at accepted weight and atmosphere. | Deaeration, nitrogen, zipper/applicator, checkweigh, cartoning. |
| Multilane sachet | Powder and printed multilane film. | Separated leak-tight sachets with controlled per-lane dose. | Registration, gas, counting, bundling and cartoning. |
| Hygienic bulk bag | Powder, liner/FIBC and permitted pallet arrangement. | Weighed, densified, closed liner/bag ready for transfer. | Bag inflation, nitrogen, sampling, airlock and palletizing. |
Milk Powder Can Filling and Seaming
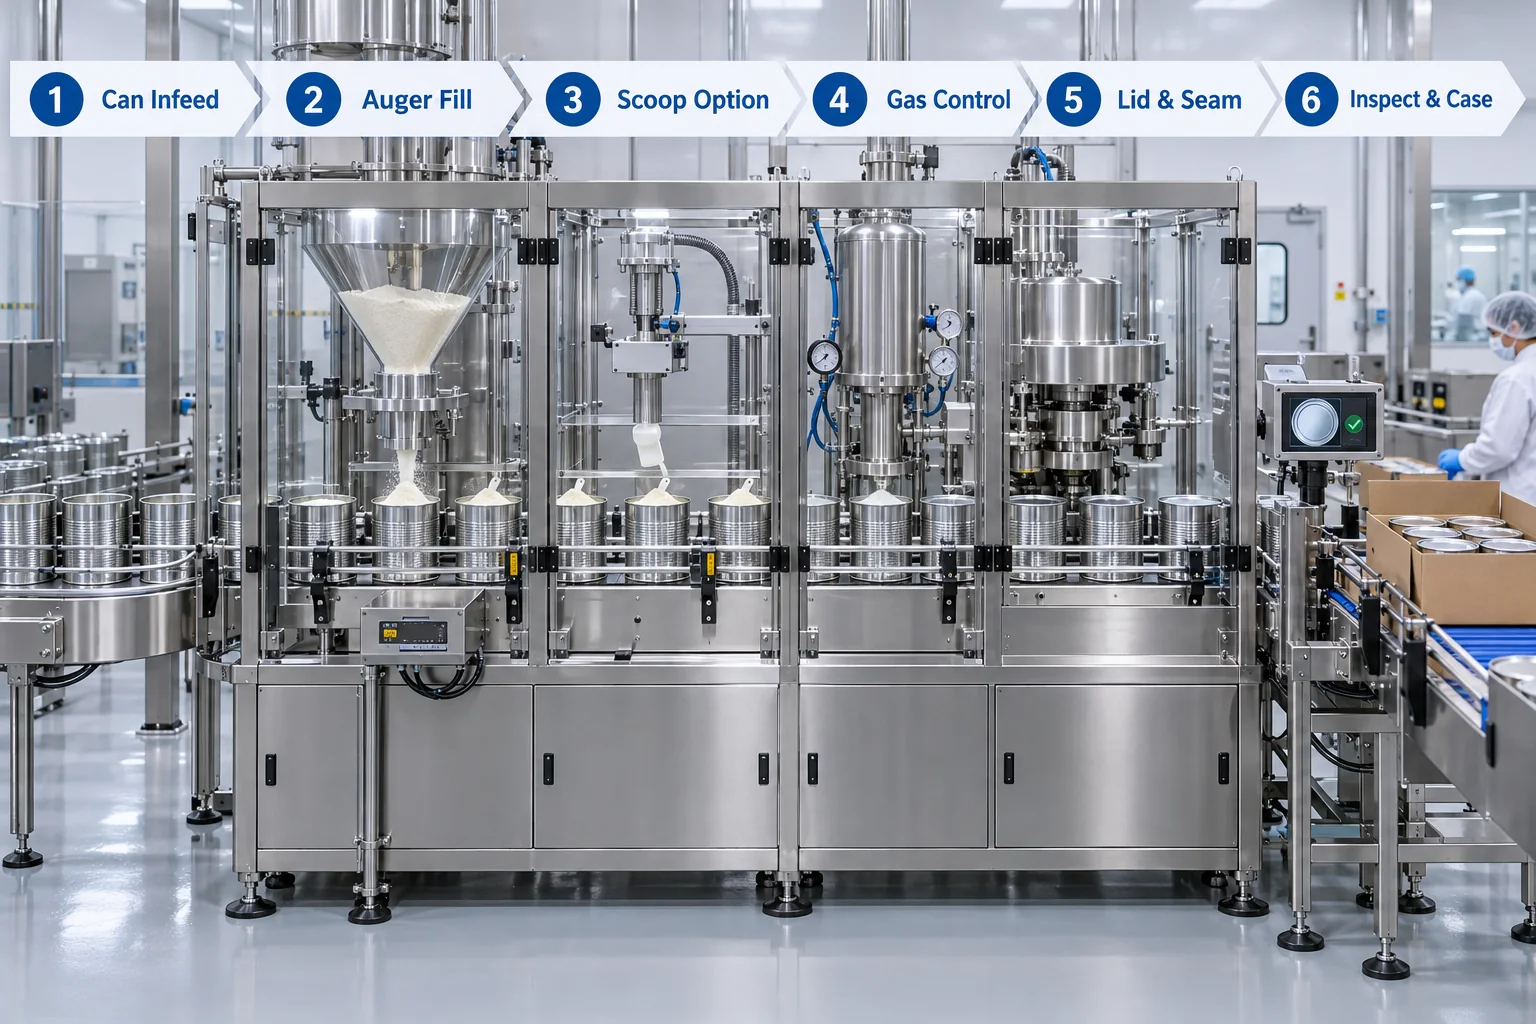
Qualified empty cans enter the high-care packaging area and reach the powder filler. A coarse/fine auger or weighing strategy controls the dose. If a scoop is required, define whether it is placed before, during or after filling and how the system prevents rim contamination. The atmosphere step may use vacuum, nitrogen displacement or another validated method before the lid is placed and the seam is formed.
Can seaming is a mechanical closure process with measurable seam geometry. Residual oxygen and seam integrity are different controls: acceptable gas results cannot compensate for an unacceptable seam, and a good seam does not prove the target atmosphere.
| Item | Provide | Acceptance evidence |
|---|---|---|
| Can/end | Material, diameter, height, flange/end profile and supplier drawings. | Stable handling and seam dimensions within the approved specification. |
| Powder dose | Net weight, bulk-density range, headspace and tolerance. | Coarse/fine fill achieves accepted weight without rim contamination. |
| Scoop | Dimensions, material, orientation and insertion point. | Correct presence and position without damaging closure or hygiene. |
| Gas process | Gas quality, sequence, pressure/flow and residual target/sample time. | Closed-can headspace result by the agreed analyzer method. |
| Seam | Seamer tooling, chuck/roll setup and inspection frequency. | Teardown measurements, visual checks and leak performance pass. |
Retail Pouch VFFS
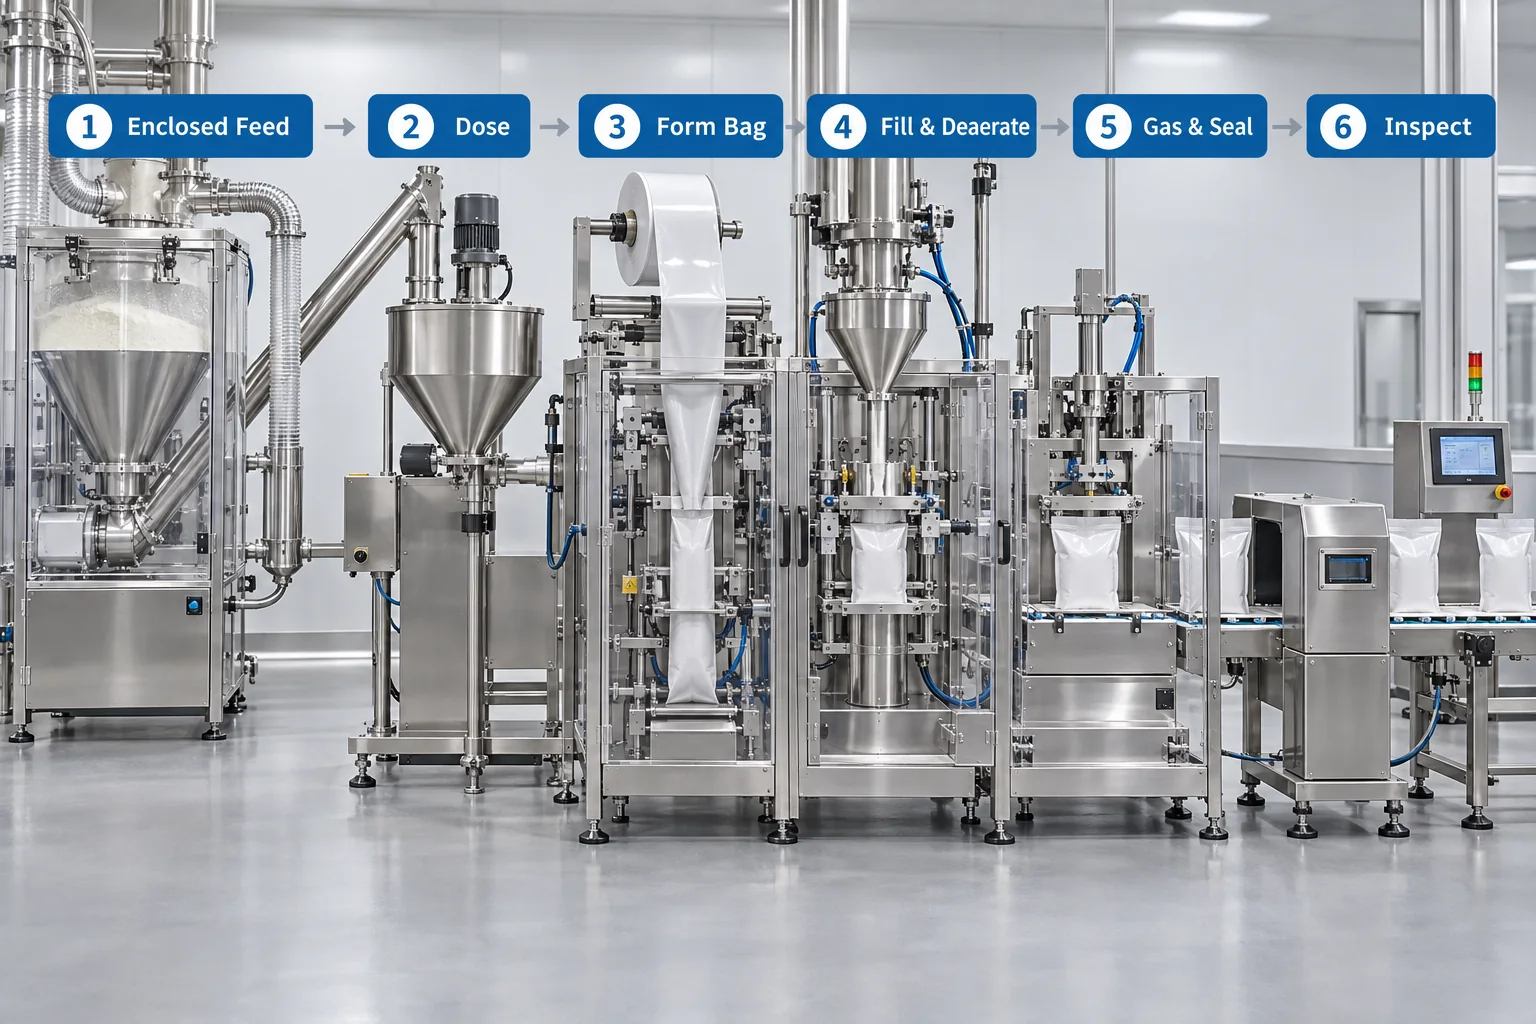
A VFFS line draws barrier film over a forming shoulder, creates the longitudinal seam and bottom seal, then doses milk powder into the bag. Bottom-up filling or controlled bag lowering can reduce drop and entrained air for suitable configurations. The top seal must remain clear of dust; extraction should capture airborne powder without removing product or disturbing weighing.
Gas flushing is included only when the product specification requires it. Validate the gas delivery, purge time, powder displacement and residual oxygen in the sealed pouch after the agreed equilibration period.
| Area | Define | Failure if ignored |
|---|---|---|
| Film roll | Barrier structure, thickness, width, core, diameter, sealant and winding. | Poor forming, weak seals, unsupported reel or moisture/oxygen exposure. |
| Print/bag | Eye mark, repeat, gusset/block bottom, dimensions and easy-open feature. | Misregistered artwork, wrong cut or unstable retail pack. |
| Powder fill | Dose, density range, drop, venting/deaeration and dust extraction. | Inflated bags, weight drift and powder in the seal. |
| Gas/atmosphere | Validated gas, delivery point, target and test timing. | False confidence from gas flow without sealed-pack verification. |
| Discharge | Bag settling, checkweigh, metal detection and carton pattern. | Seal stress, pileup or downstream bottleneck. |
Sachets and Hygienic Bulk Bags
Multilane sachet machines distribute powder across several dosing paths. The total headline output matters less than accepted dose and seal performance in every lane. Check lane-to-lane balance and trace each reject to the source lane.
Bulk milk powder needs dust-tight spout connection, supported weighing and controlled bag settling. High-care plants may keep wooden pallets outside the filling room and move the sealed bag through an airlock before palletizing. The hygiene zoning and liner-sealing sequence must match the facility design.
| Format | Key configuration | Acceptance focus |
|---|---|---|
| Single-lane sachet | Servo auger, printed film registration, seal/cut and coder. | Dose, clean seals and changeover for each small format. |
| Multilane sachet | Independent feed balance, manifolds/augers and lane identification. | Every lane passes weight, seal and code criteria at total line rate. |
| Open-mouth 10–25 kg bag | Dust-tight clamp, gross/net weigh fill, deaeration and heat seal/sewing as specified. | Stable bag, correct weight, controlled dust and verified inner closure. |
| FIBC/bulk bag | Hygienic docking, suspended/gross weighing, vibration and liner closing. | No cross-contamination, secure liner/bag and safe transfer to pallet. |
Nitrogen and Residual Oxygen
| Control | Define | Verification |
|---|---|---|
| Gas supply | Food-grade specification, purity, dew point, pressure and flow. | Supplier certificate and monitored utility condition. |
| Sequence | Pre-flush, during-fill, post-fill, vacuum/replacement and closing timing. | Repeatable cycle under minimum/maximum line conditions. |
| Headspace/product | Fill level, powder aeration, headspace and gas displacement. | Closed-pack result after an agreed stabilization period. |
| Residual oxygen | Target, sampling location, instrument, calibration and sample plan. | Measured sealed-pack value with rejects and corrective action defined. |
| Safety | Ventilation, oxygen-deficiency assessment and alarms where required. | Site-approved gas installation and operator procedure. |
Milk Powder Packing Machine Price
The applicable Comwin budget depends on packaging route. These are planning references, not binding offers. A can filler plus seamer and gas system is not comparable with a standalone auger or VFFS bagger. Indian prices and visibly low-price marketplace products are excluded.
| Comwin reference | Planning price | Scope interpretation |
|---|---|---|
| Retail pouch or suitable powder VFFS | US$5,000–30,000. | Bagger reference; auger, feeding, gas control, dust extraction and inspection must be itemized. |
| Premade pouch machine | US$10,000–45,000. | Pouch handling and closing; powder filler, gas and zipper requirements affect scope. |
| Can filling/seaming project | Quote-based; nearest filling-and-closing reference US$12,000–50,000. | Not a fixed can-line price. Powder auger, scoop, gas, lid handling, seamer and inspection require configuration. |
| Hygienic bulk-bag system | Quote-based. | Bag docking, legal/gross weighing, dust extraction, densification, liner sealing, room/airlock and pallet handling set the budget. |
| Coordinated filling or bagged-product line | US$80,000–500,000+. | May include feeding, primary packer, gas, inspection, cartoning/case packing, conveyors and pallet handling. |
Request separate prices for powder feed, auger/weigher, packer, gas generation or mixing, dust extraction, can/scoop/lid handling, seamer, coder, residual-oxygen tester, checkweigher, metal detector, case packer, spares, FAT, freight, installation and taxes.
Hygiene and Powder Safety
| Area | Define | Design effect |
|---|---|---|
| Product contact | Materials, finish, removable parts, seals and dead spaces. | Hygienic construction, access and documented inspection. |
| Cleaning | Dry clean, COP or validated wet-clean sequence and dry-out. | Component removal, drainage, moisture control and downtime. |
| Dust extraction | Pickup points, airflow, filter return/disposal and balance. | Enclosure, containment and protection of dose/seal performance. |
| Hazard classification | Powder explosibility data, zone/class and site standard. | Grounding, electrical/mechanical protection, venting/isolation as engineered. |
| High-care zoning | People/material flow, pallet policy, airlocks and pressure concept. | Machine layout, bag/can entry and closed-pack exit. |
Weight, Atmosphere and Closure Verification
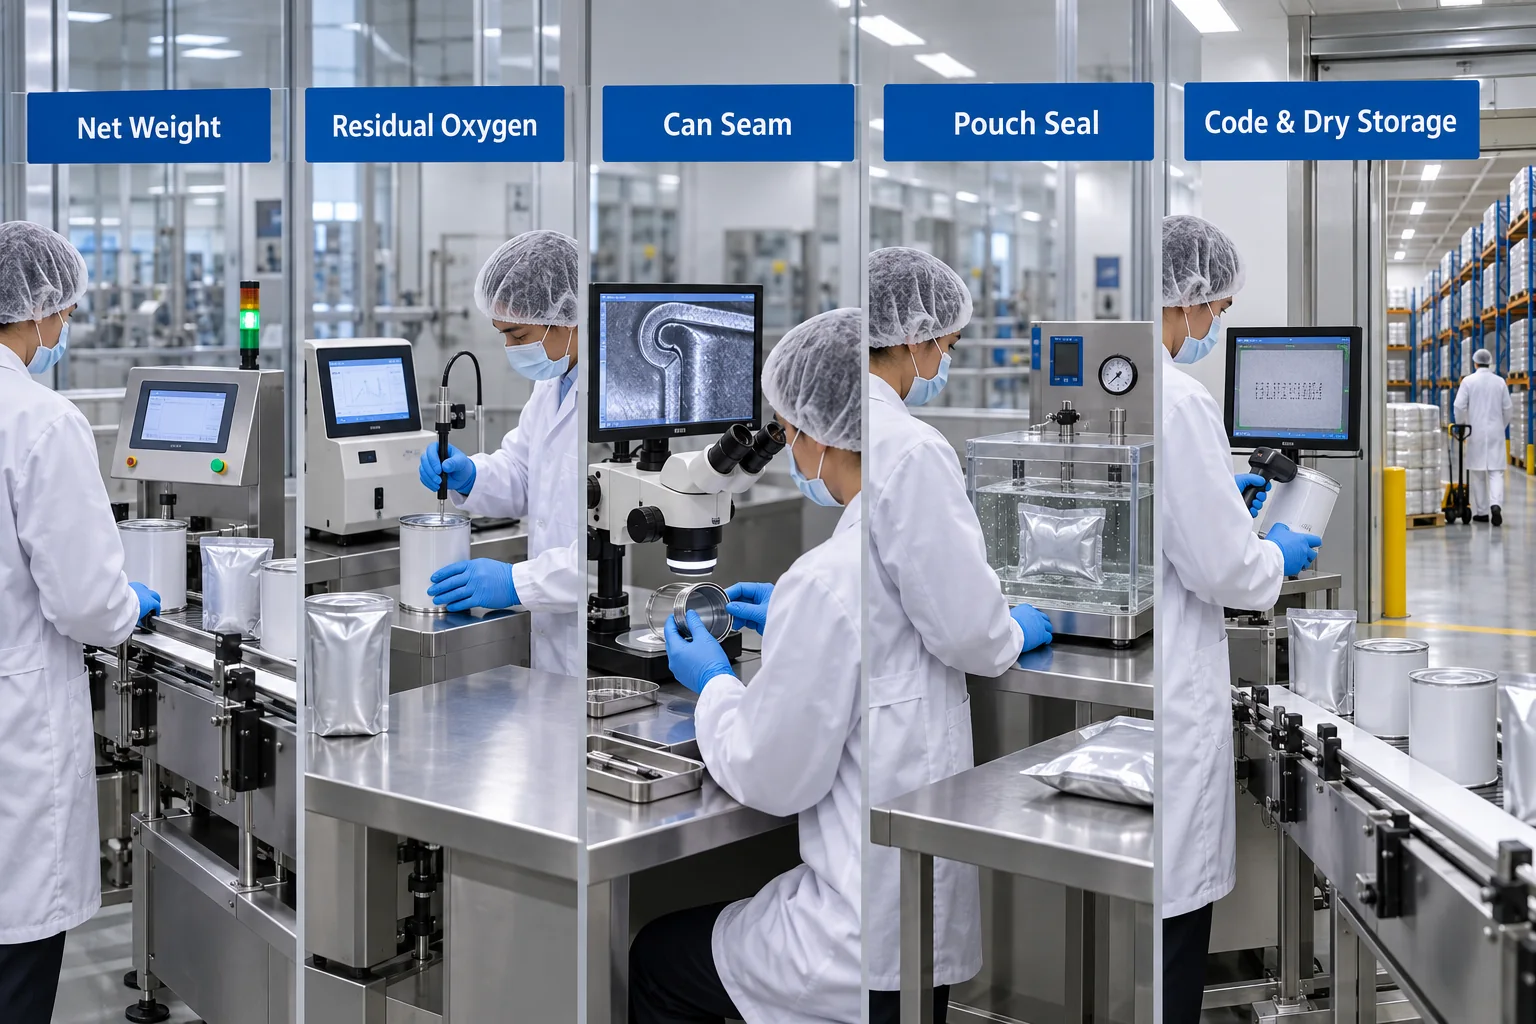
Release testing must reflect the chosen package. Cans need weight, residual oxygen when specified, seam teardown and leak checks. Pouches need weight, seal inspection, leak testing and atmosphere measurement when used. Codes, scoop presence, metal detection and dry storage conditions are separate controls.
| Check | Method | Pass condition |
|---|---|---|
| Net weight | Calibrated sampling or checkweigher by format/lane. | Within tolerance without systematic drift or excess giveaway. |
| Atmosphere | Calibrated residual-O₂ analysis after defined stabilization. | Meets product-specific target with sampling and reject plan. |
| Can seam | Visual inspection, teardown measurements and validated leak test. | Approved seam geometry and package integrity. |
| Pouch/sachet seal | Seal-area inspection plus validated leak/burst method. | No dust channel, wrinkle or recurring failure. |
| Code/storage | Vision/operator code verification and humidity/temperature records. | Readable traceability and storage within validated conditions. |
Quotation and FAT Inputs
| Input | Provide | Quotation effect |
|---|---|---|
| Powder | Type, fat/moisture, particle range, loose/settled density, flow and dust data. | Defines hopper, transfer, dosing, extraction, cleaning and safety. |
| Pack | Can/end/scoop, film roll, sachet web or bulk bag/liner samples and drawings. | Defines handling, tooling, forming and closing. |
| Formats | Fill weights, dimensions, headspace and number of SKUs. | Defines auger/weigher range, recipes and change parts. |
| Atmosphere | Gas specification, residual target, sampling time and shelf-life protocol. | Defines gas/vacuum system, sensors and inspection. |
| Output | Accepted packs/hour by format/lane and shifts. | Defines filler count, lane/cavity count and downstream capacity. |
| Factory/final pack | Utilities, zoning, layout, code, carton/case and pallet plan. | Defines interfaces, documentation, conveyors and project boundary. |
Send representative powder and package materials for free sample testing. FAT should cover start-up, steady output, refill, normal stop/restart, format change and cleaning using written weight, atmosphere, seal/seam, reject and accepted-output criteria.
Supplier Positioning
| Supplier / region | Positioning | Evaluation focus |
|---|---|---|
| Comwin Group / China | Customized powder VFFS, pouch, can and coordinated end-of-line project matching. | Sample testing, correct package route, itemized scope and one project boundary. |
| Chinese export market | Wide choice of auger fillers, can/gas/seaming lines and sachet/VFFS systems. | Hygienic details, dust control, components, production-material FAT, documents and support. |
| Rovema / Europe and North America | Industrial powder VFFS, gas flushing and bulk bagging platforms. | Deaeration, residual oxygen, seal cleanliness, film range and regional service. |
| GEA / Europe and global | High-care dairy powder and FIBC filling systems. | Room concept, hygienic docking, pallet separation, filling density and lifecycle support. |
| Premier Tech / North America and global | Hygienic open-mouth bottom-up powder filling. | Dust/aeration reduction, bag formats, weighing and site integration. |
Frequently Asked Questions
Which filler is best for milk powder?
A servo auger is a common starting point for retail cans, pouches and sachets. Net-weight or combined systems suit projects where direct weight control, bulk filling or density variation justifies the added scale and feed controls.
Can one machine pack cans and pouches?
Not as one primary machine. The powder feeder or filler concept may be related, but cans require lid placement and seaming while pouches require film forming and heat sealing. Treat them as separate lines or changeover modules only after engineering review.
How much does a milk powder packing machine cost?
Comwin VFFS is US$5,000–30,000. Can and hygienic bulk-bag systems are quote-based; US$12,000–50,000 is only the nearest filling-and-closing reference. Coordinated lines are generally US$80,000–500,000+.
Does a nitrogen connection prove low residual oxygen?
No. Validate gas quality, sequence, headspace, line speed and the residual oxygen measured in sealed packs after an agreed stabilization time.
How do I stop milk powder from contaminating pouch seals?
Control auger cutoff, drop height, deaeration, dust extraction, bag length and jaw timing. Test the most aerated production powder at commercial speed and inspect the top seal for channels.
Request a Milk Powder Packaging Proposal
Send your powder data, package samples, fill weights, atmosphere specification, accepted output and factory zoning through our contact page. Comwin provides the most suitable packaging solution for your product, pack format and production requirements. Service includes a two-year machine warranty, three-year core-component warranty and remote response within 24 hours.